Content
Precision harmonic reducer bearings are critical components in motion-control systems that demand high rigidity, accurate rotation, compact dimensions, and dependable service life. They are used in harmonic drive mechanisms serving robotics, machine tools, aerospace equipment, intelligent automation, and other applications where even a small amount of backlash, deflection, or rotational error can influence the performance of the complete machine.
A harmonic reducer bearing does not operate as an isolated rolling element product. It works as part of a precision transmission assembly that includes a harmonic generator, a flexible element, a rigid wheel, a rigid bearing, and a flexible bearing. Each component must cooperate with the others under demanding mechanical conditions. The bearing must therefore provide more than ordinary rotation. It must support structural loads, preserve alignment, withstand repeated deformation or eccentric loading, and maintain predictable performance throughout the operating cycle.
UKL Bearing Manufacturing Co., Ltd. supplies precision harmonic reducer bearings designed for these requirements. The company integrates research and development, forging, turning, heat treatment, grinding, assembly, inspection, packaging, and international distribution. This integrated manufacturing structure allows the production process to be controlled from material preparation through final delivery, helping customers obtain consistent components for robotic joints, precision reducers, and other compact transmission systems.
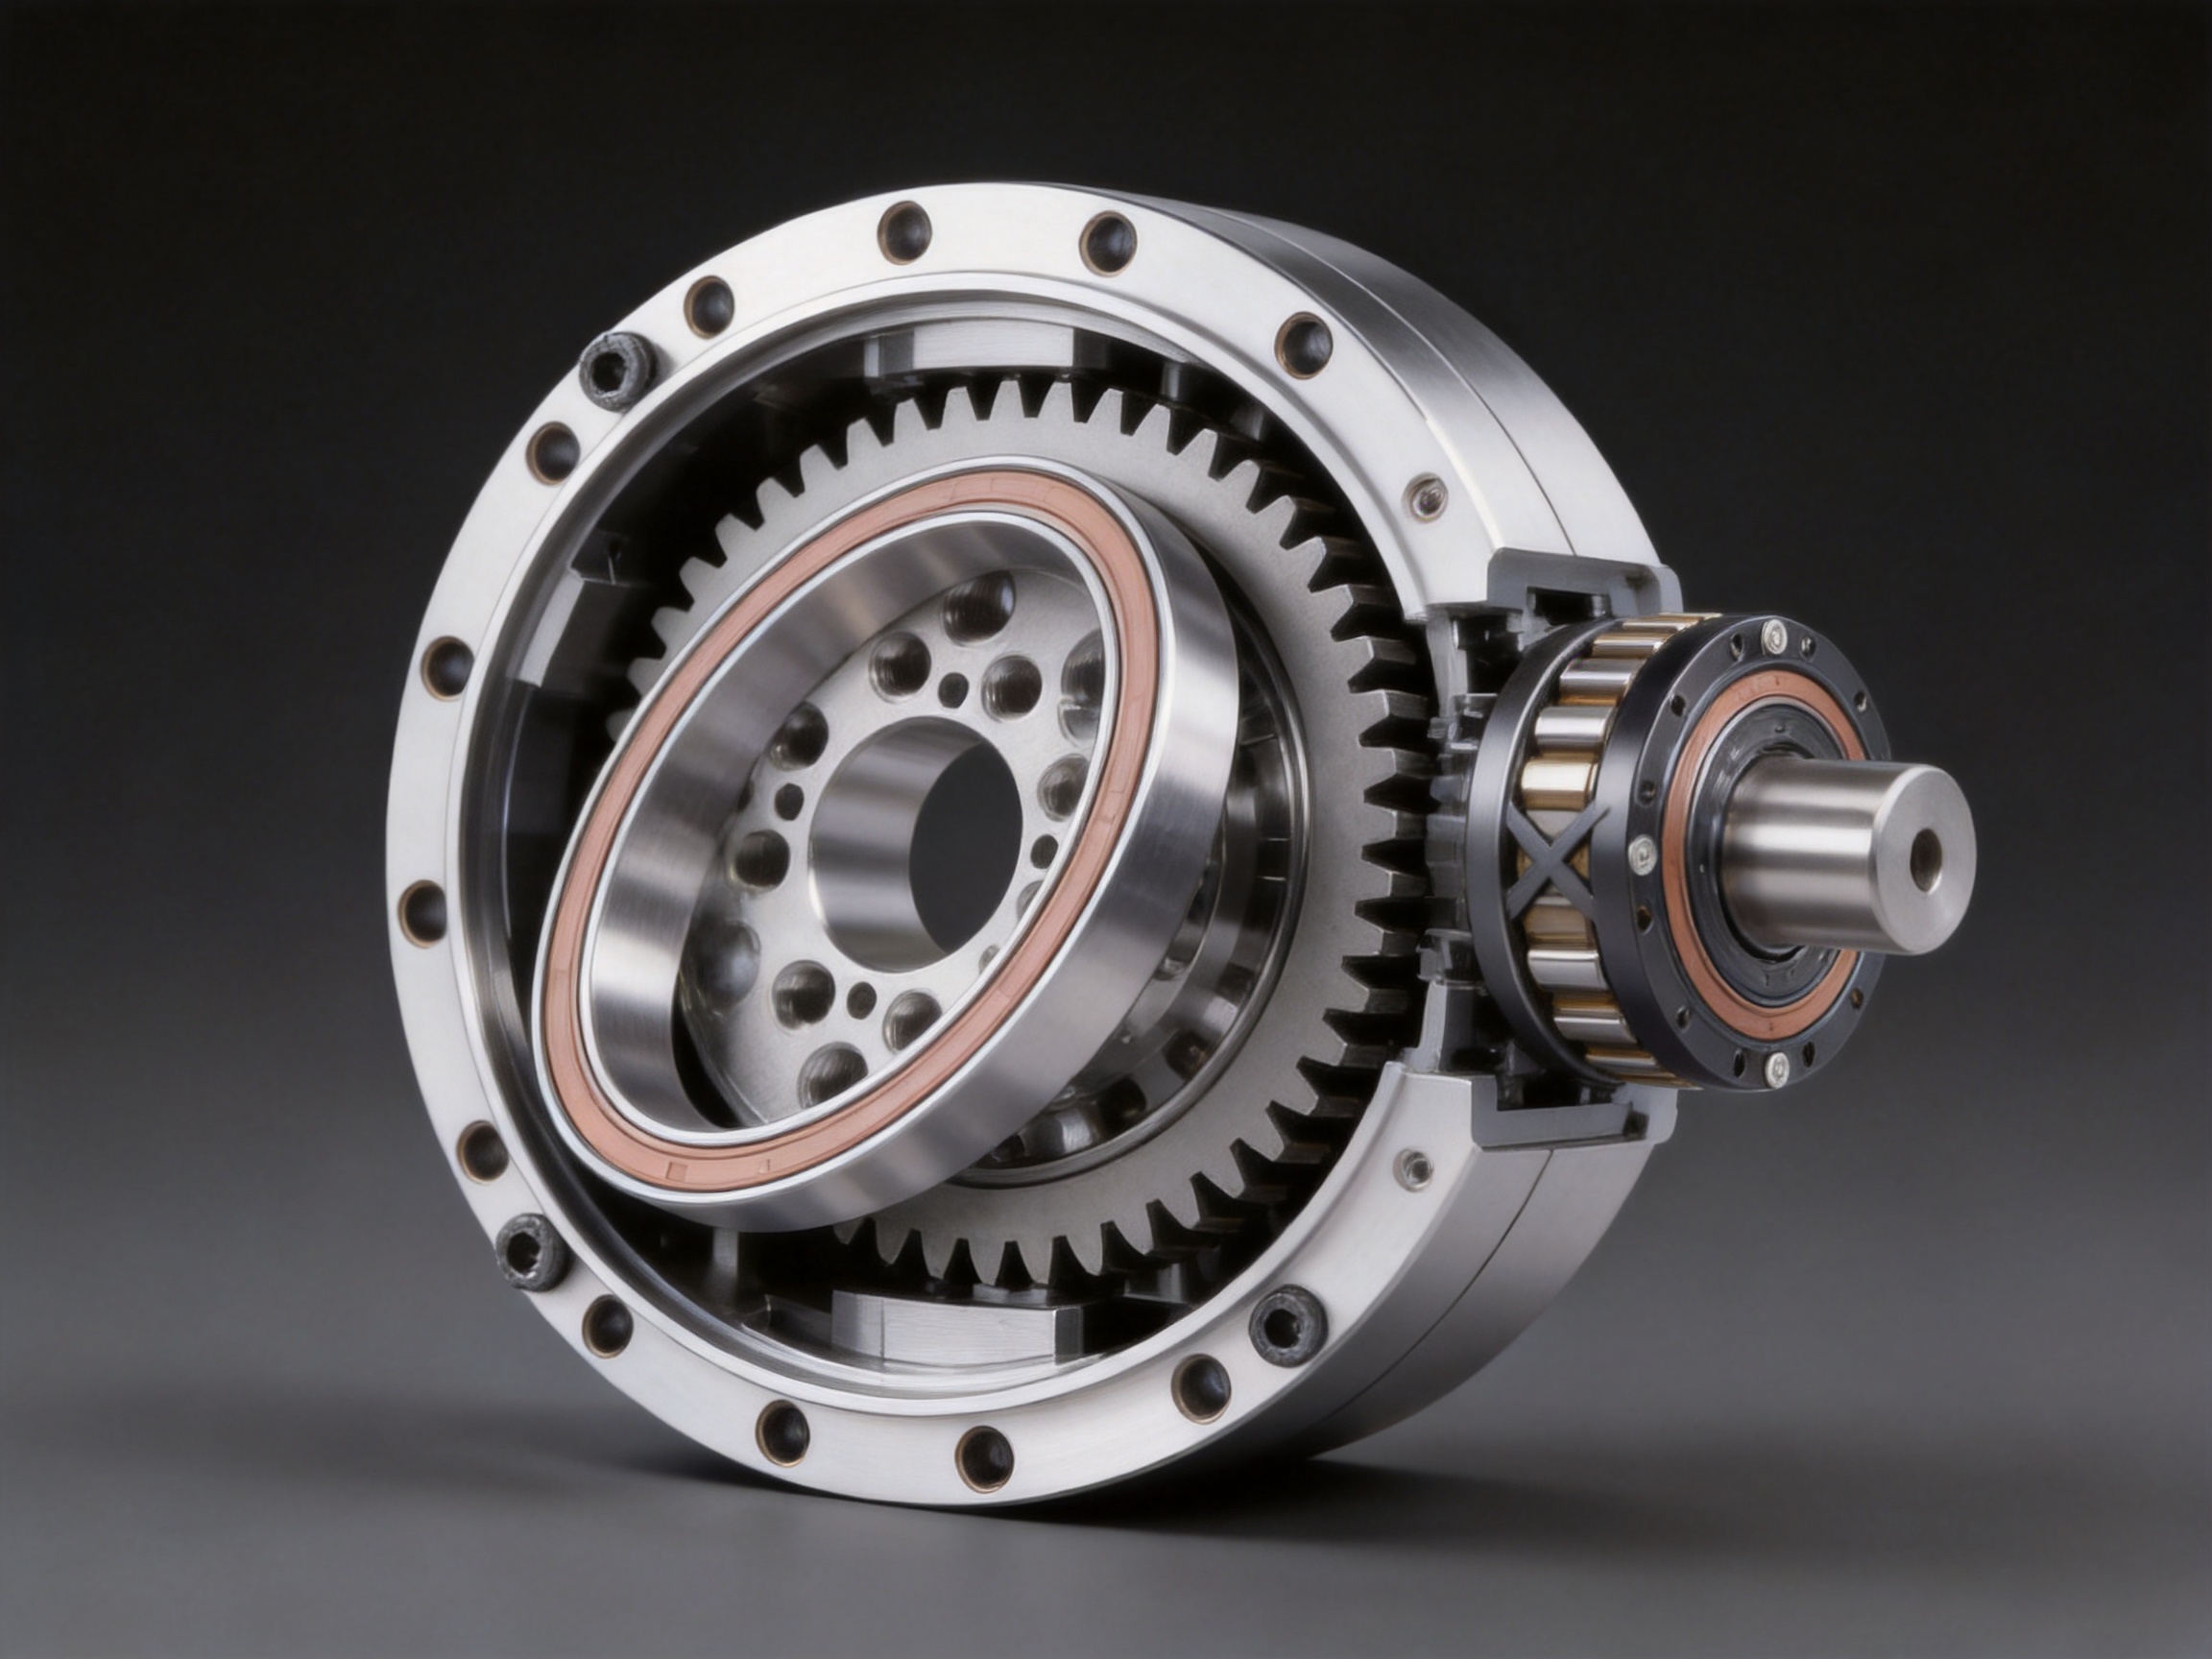
A harmonic reducer is based on controlled elastic deformation and tooth engagement. Its principal components are commonly identified as the harmonic generator, the flexure, and the rigid wheel. The assembly also uses a rigid bearing, often a crossed roller bearing, together with a flexible bearing that is commonly a thin-walled deep groove ball bearing.
The harmonic generator contains an elliptical cam. The inner bore of the flexible bearing fits over the outer surface of this cam. As the cam rotates, the flexible bearing is forced into an elliptical shape. The outer ring of the flexible bearing deforms elastically through the action of the rolling elements and transfers this shape to the opening of the flexure.
The outside circumference of the flexure contains gear teeth. These teeth engage with the internal teeth of the rigid wheel. The rigid wheel has more teeth than the flexure. Because of this difference, engagement occurs along the long axis of the elliptical form, while disengagement occurs near the short axis. The resulting tooth movement creates a large reduction ratio in a compact package.
The lower portion of the flexure is fixed to the output end, while the rigid bearing is installed at the output end of the reducer for connection with an external load or mechanism. In this arrangement, the bearing is exposed to a combination of radial loading, axial loading, overturning moment, and repeated rotational movement. The bearing must maintain the relationship between the reducer components while allowing smooth, accurate output rotation.
This operating principle explains why ordinary commercial bearings may not be suitable for every harmonic reducer. A bearing designed only for conventional radial rotation may not provide the stiffness, mounting accuracy, or load distribution required by a compact reducer. Harmonic drive bearings must be selected and manufactured according to the geometry, preload, load direction, installation method, and duty cycle of the complete transmission.
Robotic joints and automated positioning systems often repeat the same motion thousands or millions of times. A slight change in bearing clearance, raceway accuracy, or mounting alignment can gradually become visible as positioning error, vibration, noise, or increased power consumption. In a harmonic reducer, the bearing also influences the stability of the flexure, the rigid wheel, and the output flange.
For rigid bearings, the most important performance indicators generally include rigidity, reliability, and rotational accuracy. A rigid bearing with insufficient stiffness can allow unwanted movement between the reducer and the output load. This movement may appear as angular deflection under torque or as reduced positioning repeatability during acceleration and deceleration.
Preload is typically applied before shipment to improve rigidity and control internal clearance. Correct preload supports a stable rolling contact condition and reduces unwanted movement between the rolling elements and raceways. However, preload must be carefully controlled. Excessive preload increases friction, heat generation, and torque, while insufficient preload may reduce stiffness and allow vibration or displacement.
For flexible bearings, maximum radial deformation is a core performance parameter. The flexible bearing must accommodate the elliptical deformation generated by the cam without premature raceway damage, excessive torque, or loss of rolling contact. Its thin-walled structure requires careful control of material quality, heat treatment, grinding accuracy, internal clearance, and assembly conditions.
Precision manufacturing is therefore connected directly to reducer performance. Dimensional tolerances, roundness, waviness, raceway geometry, surface roughness, rolling-element quality, cage design, lubricant compatibility, and sealing or protection requirements all contribute to the final result. A bearing supplier must understand how these factors interact instead of treating the bearing as a standard catalog item.
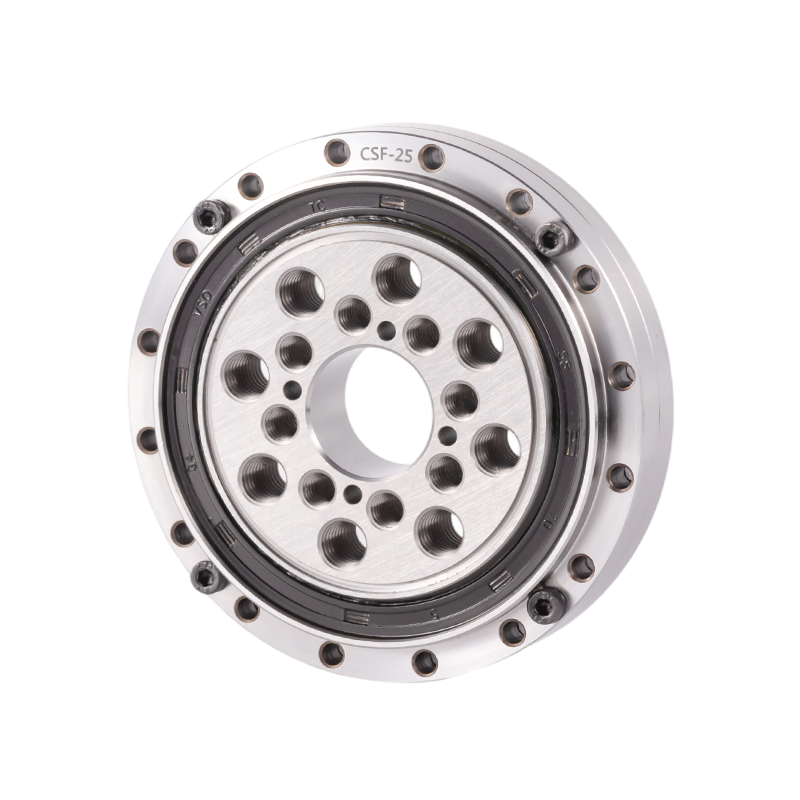
Precision Harmonic Reducer Bearing
The rigid bearing supports the output-side structure and provides the mechanical interface between the reducer and the external machine. It must resist radial and axial forces while maintaining the geometric relationship of the output components. In robotic joints, the rigid bearing may also support an external arm, tooling system, or payload that generates a substantial overturning moment.
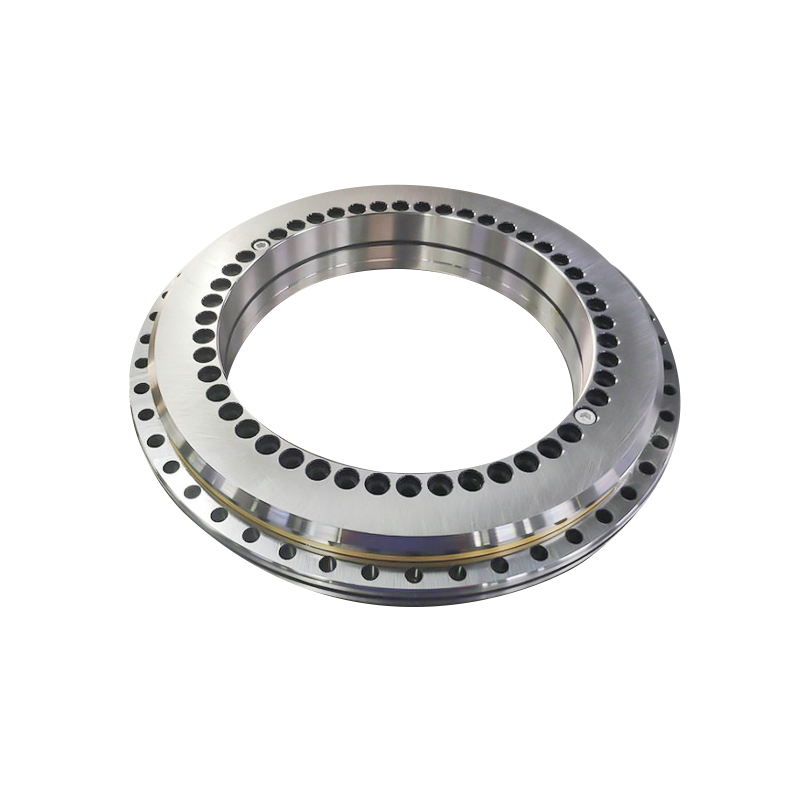
A crossed roller bearing is frequently used for this role because its rollers are arranged alternately at right angles. This arrangement allows the bearing to carry radial loads, axial loads, and moment loads in a compact cross section. The load is distributed across multiple rollers, supporting high rigidity without requiring a large bearing diameter.
Compared with a conventional deep groove ball bearing of similar external dimensions, a crossed roller bearing can provide a more direct structural connection and improved resistance to tilting. This characteristic is valuable in robot joints and rotary tables where the output load is not centered over the bearing. The bearing can help reduce the amount of additional support structure required around the reducer.
The flexible bearing operates under repeated elliptical deformation. Its inner bore mates with the harmonic generator cam, while its outer ring interacts with the flexure. The bearing must tolerate the deformation produced by the eccentric or elliptical cam while keeping rolling resistance under control.
The flexible bearing requires a carefully balanced design. A thin wall allows the necessary deformation, but it also reduces the structural margin available for resisting damage. High-quality steel, controlled heat treatment, precise raceway grinding, and accurate rolling-element selection are important for achieving a reliable balance between flexibility and fatigue resistance.
Because the flexible bearing is subject to a distinctive operating pattern, its performance should be evaluated according to the actual reducer design. Radial deformation, rotational speed, transmitted torque, lubrication, temperature, installation fit, and operating frequency should all be considered. A bearing that performs well in a conventional application may not be the best choice for a harmonic drive if it cannot tolerate the required deformation cycle.
Harmonic reducers are valued for their high reduction capability and compact architecture. The associated bearings must preserve this advantage. A suitable bearing should deliver load capacity and rigidity without adding unnecessary radial or axial space.
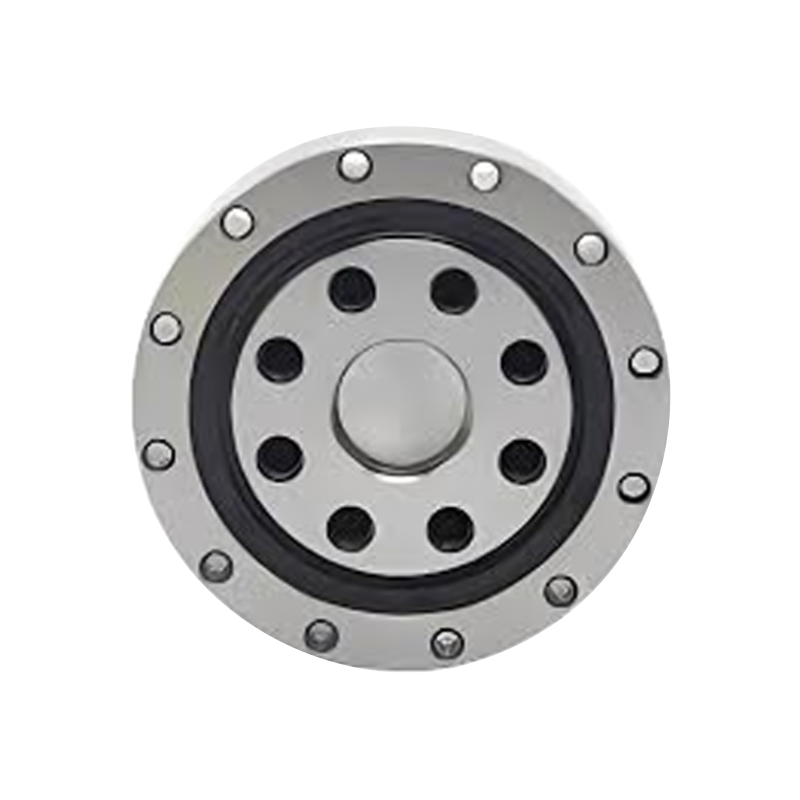
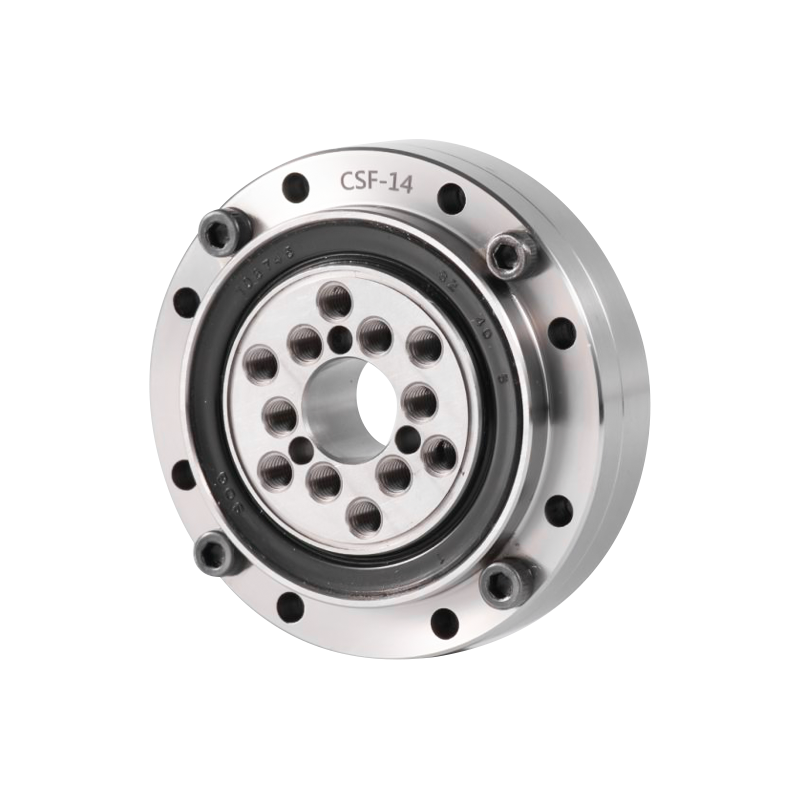
The listed CSF(G) series dimensions cover several size classes, from the compact CSF(G)-14 and CSF(G)-17 models to the larger CSF(G)-65 model. This range allows designers to match the bearing to different reducer sizes, robot joint capacities, and mounting arrangements. The sizes also use distinct installation hole patterns and threaded specifications to support integration with corresponding reducer housings and output structures.
The following values are the supplied overall and installation dimensions for the precision harmonic reducer bearing range. The notation includes the primary outside diameter D, bore diameter d, section dimensions C, H, and B, pitch-circle diameter dm, installation hole specification, and weight. Because mounting requirements can vary according to reducer design, customers should confirm the complete drawing and tolerance requirements before production.
| Bearing Type | D (mm) | d (mm) | C (mm) | H (mm) | B (mm) | dm (mm) | Mounting Specification | dn (mm) | Mounting Specification | Weight (kg) |
|---|---|---|---|---|---|---|---|---|---|---|
| CSF(G)-14 | 55 | 11 | 16 | 16.5 | 13.5 | 49 | 8-φ3.5 | 23 | 6-M4 | 0.15 |
| CSF(G)-17 | 62 | 10 | 16 | 16.5 | 13.5 | 56 | 10-φ3.5 | 27 | 6-M5 | 0.24 |
| CSF(G)-20 | 70 | 14 | 16 | 16.5 | 13.5 | 64 | 12-φ3.5 | 32 | 8-M6 | 0.30 |
| CSF(G)-25 | 85 | 20 | 18 | 18.5 | 16.5 | 79 | 16-φ3.5 | 42 | 8-M8 | 0.45 |
| CSF(G)-32 | 112 | 26 | 21.5 | 22.5 | 19 | 104 | 16-φ4.5 | 55 | 8-M10 | 0.90 |
| CSF(G)-40 | 126 | 24/32 | 22.5 | 24 | 21.5 | 117 | 20-φ5 | 68 | 8-M10 | 1.30 |
| CSF(G)-50 | 157 | 32/40 | 30 | 31 | 28 | 147 | 16-φ5.5 | 84 | 8-M14 | 2.80 |
| CSF(G)-65 | 210 | 44/52 | 37 | 39 | 35 | 198 | 20-φ6.5 | 110 | 8-M16 | 7.90 |
The table demonstrates the scalable nature of the product family. As the bearing size increases, the outside diameter, section dimensions, mounting pitch-circle diameter, and weight also increase. This progression allows equipment manufacturers to select an appropriate size while preserving the basic integration concept across multiple reducer platforms.
Some models use two alternative bore dimensions, such as CSF(G)-40, CSF(G)-50, and CSF(G)-65. This provides additional flexibility for applications with different shaft or cam arrangements. The final selection should consider the reducer model, shaft interface, interference fit, mounting rigidity, available clearance, and required service conditions.
One of the principal advantages of a precision harmonic reducer bearing is its focus on structural rigidity. In a general-purpose bearing application, the primary objective may be to support a rotating shaft with a predictable radial or axial load. In a harmonic reducer, the bearing is also part of the structural body of the transmission. It must help preserve output alignment under torque and external moment loads.
The crossed roller arrangement is particularly beneficial where a compact bearing must support combined loads. Alternating roller orientation distributes load in multiple directions and helps limit tilting. This can reduce the need for separate axial or moment-supporting components, allowing the reducer to remain compact and responsive.
Rotational accuracy depends on raceway geometry, bearing roundness, rolling-element consistency, preload, mounting accuracy, and the precision of the adjacent reducer parts. A purpose-designed harmonic reducer bearing is produced with these relationships in mind.
Accurate rotation supports better positioning repeatability, smoother servo response, and reduced vibration. These advantages are important in robotic arms, semiconductor handling equipment, inspection systems, machine-tool indexing units, and precision assembly equipment. The bearing does not eliminate errors generated elsewhere in the reducer, but it provides a stable mechanical foundation for the full system.
Space is often limited inside a robotic joint. Motors, brakes, encoders, cables, reducers, and bearings must fit inside a small housing. A large conventional bearing may increase the size and mass of the joint, while separate radial and axial bearings may require additional components and assembly steps.
A crossed roller bearing can combine several load-supporting functions in one compact unit. This helps designers reduce the overall number of parts and may simplify the load path between the reducer output and the external mechanism. Lower component count can also support easier maintenance and more consistent assembly.
Preload is a major difference between a precision reducer bearing and a loose-fit general-purpose bearing. Controlled preload reduces internal movement and increases the stiffness of the bearing system. This is especially useful in servo-driven mechanisms that frequently change direction or stop at precise positions.
Preload must be matched to the intended duty. The appropriate level depends on load, speed, temperature, lubrication, mounting deformation, and expected service life. A qualified manufacturer can help determine whether a standard preload, customized preload, or application-specific adjustment is appropriate.
The CSF(G) series provides multiple diameter and bore options. This range is useful for equipment manufacturers that develop several robot sizes or reducer models. A common bearing design approach across different dimensions can simplify product development, supplier management, and maintenance planning.
Smaller models are suited to compact joints and lightweight mechanisms, while larger models can support higher external loads and larger output structures. Selection should not be based on outside diameter alone. The designer should also evaluate bearing section, mounting-hole pattern, dynamic and static load, moment load, shaft interface, expected speed, and the number of deformation cycles for the flexible bearing.
The manufacturing process begins with suitable bearing steel and controlled material preparation. Forging can improve the structural integrity of the raw ring by forming the material close to the required geometry. Proper forging practice supports a consistent grain flow and reduces the amount of material that must be removed during later machining.
Material traceability is important throughout this stage. Each production batch should be identifiable so that chemical composition, heat-treatment records, inspection results, and final assembly information can be connected. This traceability provides a foundation for quality analysis and helps the manufacturer respond efficiently if a technical question arises after delivery.
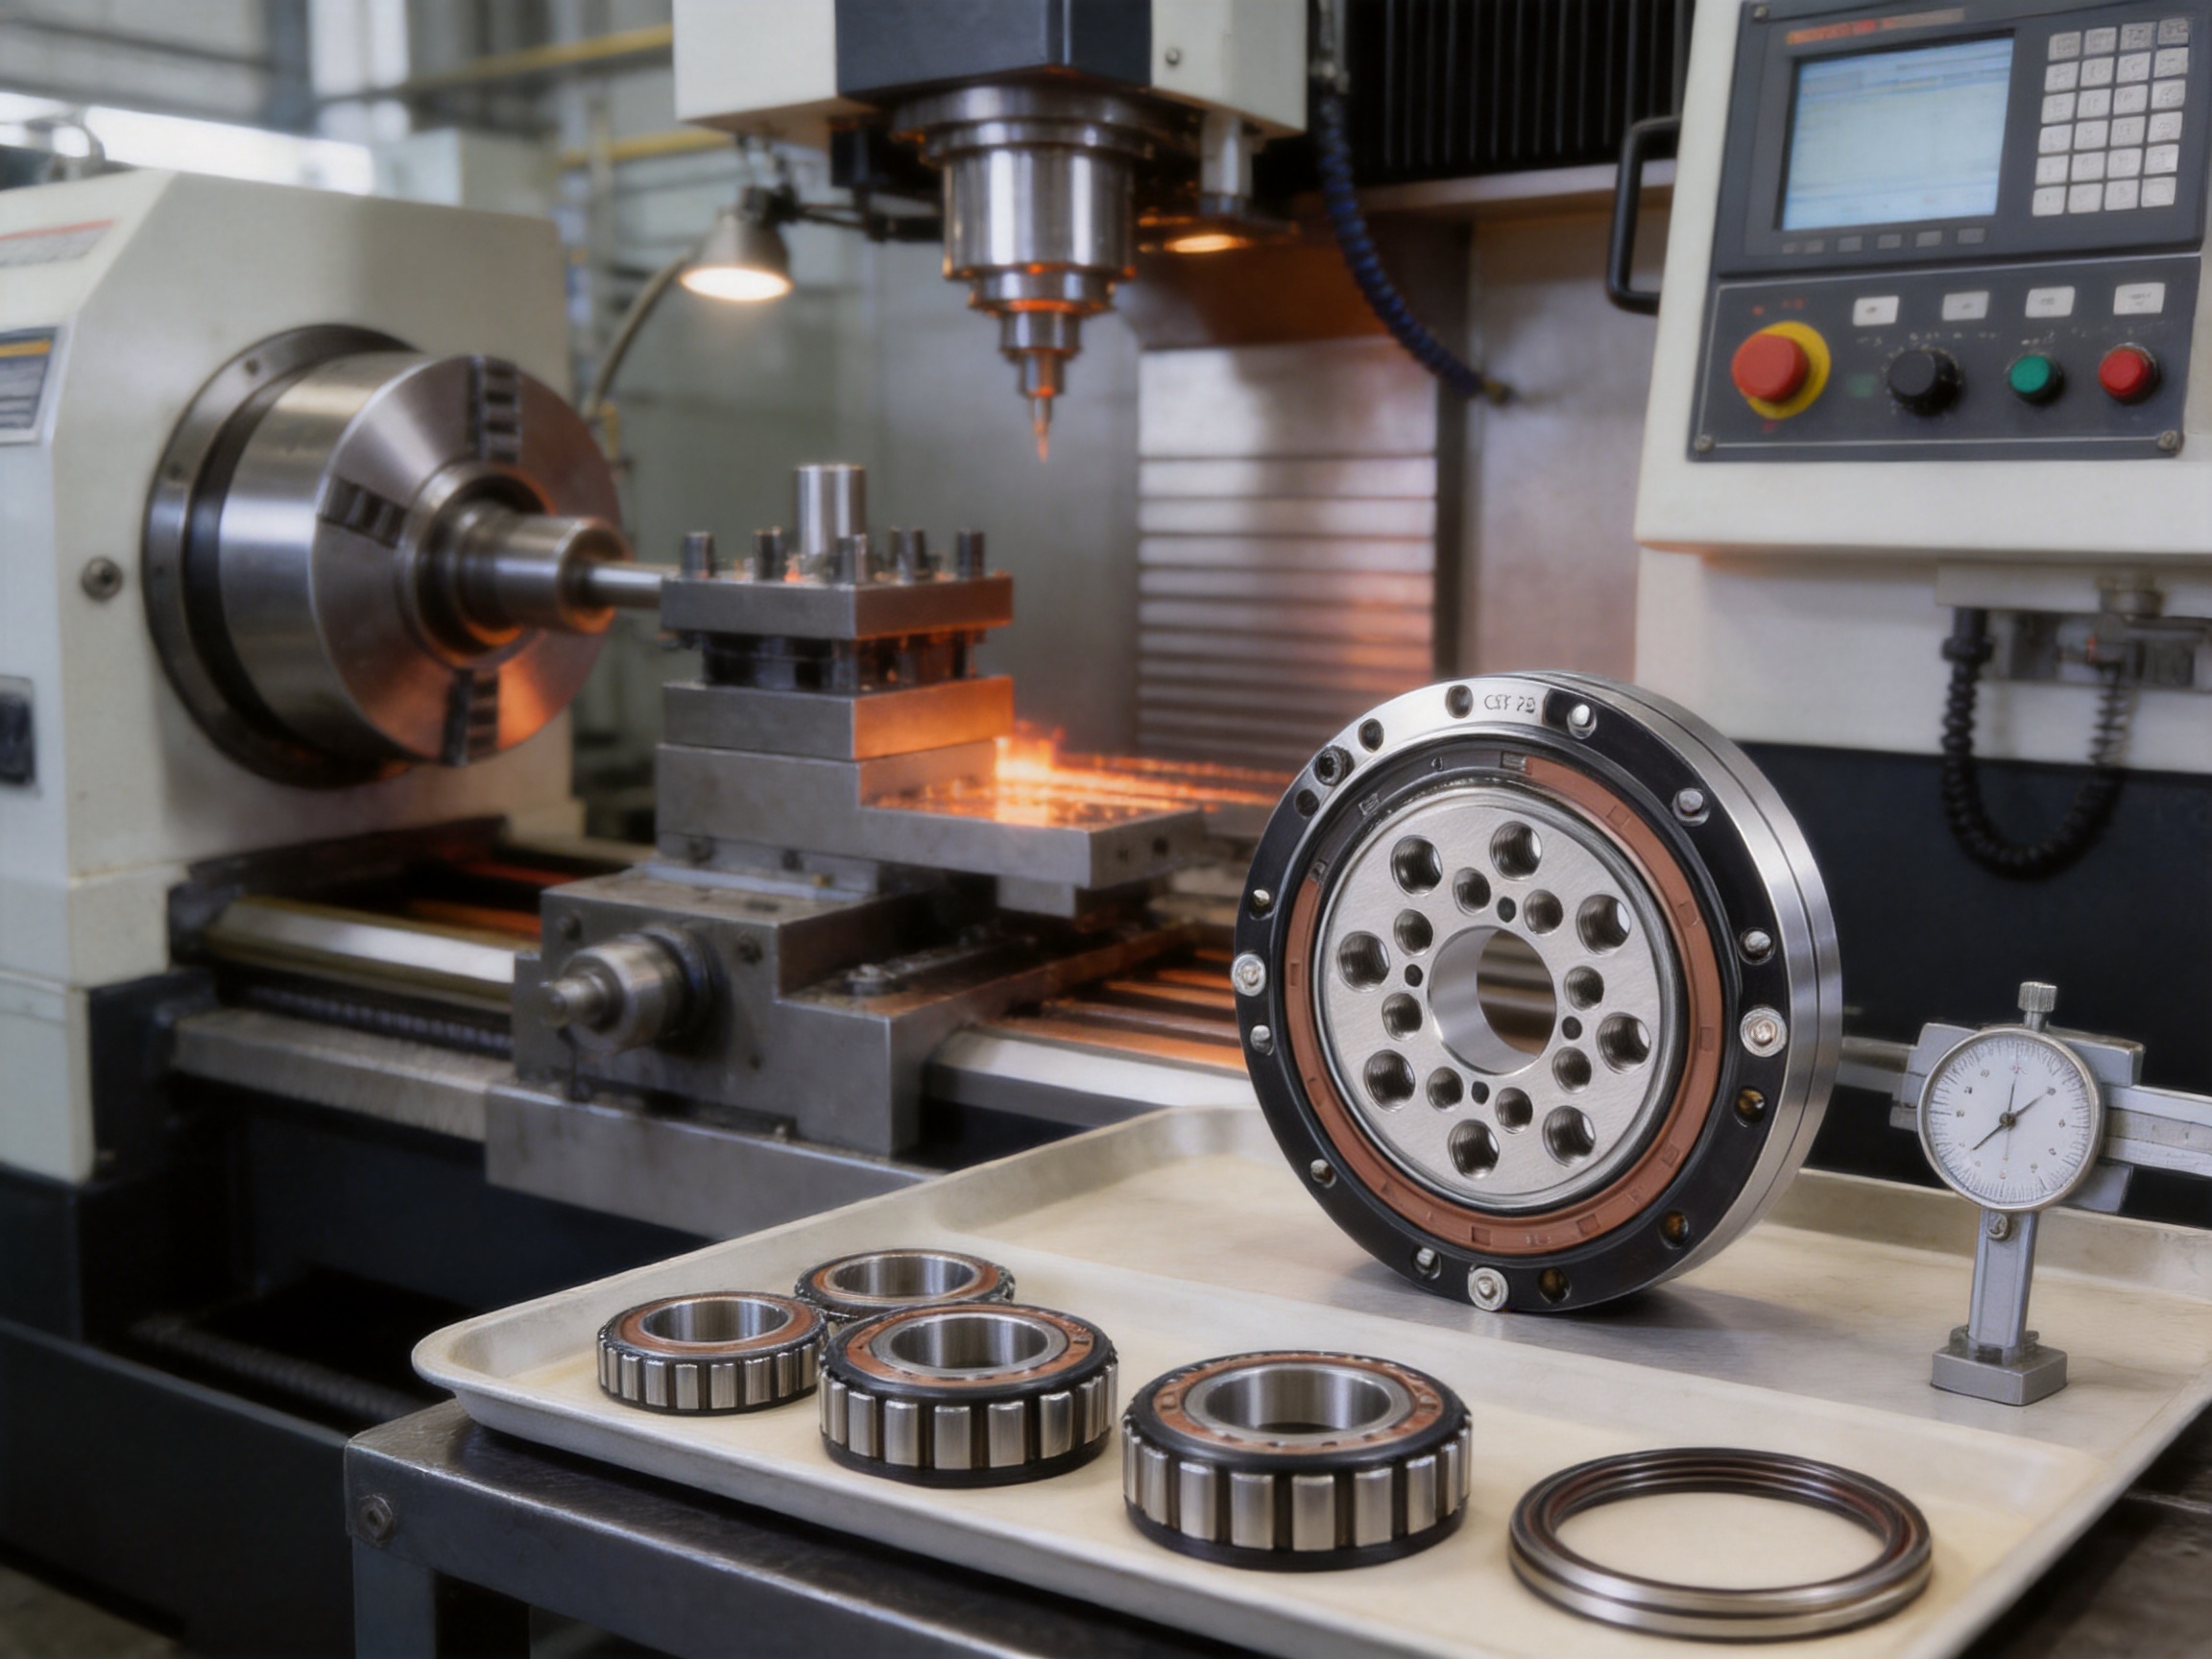
After forging, turning operations establish the main ring dimensions, reference surfaces, mounting features, and preliminary raceway geometry. Precision turning creates the foundation for subsequent heat treatment and grinding. Stable cutting conditions, suitable tooling, controlled clamping, and measurement between operations help limit distortion and maintain repeatability.
For harmonic reducer bearings, reference surfaces are particularly important. The bearing must be mounted accurately within the reducer housing and relative to the flexure, cam, and output flange. Errors introduced during turning can affect the final concentricity and axial alignment of the assembled unit.
Heat treatment gives the bearing rings the hardness, wear resistance, and fatigue strength required for rolling contact. The process must be controlled to achieve the required material properties while limiting dimensional change and residual stress.
Heat-treatment distortion is a serious consideration for thin sections and precision bearing rings. If distortion is not controlled, excessive grinding stock may be required or the final geometry may be difficult to achieve. A carefully managed process, combined with appropriate inspection, supports more stable production and better consistency between batches.
Grinding is used to achieve final raceway dimensions, geometry, and surface quality. Bearing raceways must be smooth and accurately formed because rolling contact is sensitive to waviness, roughness, and profile error. Grinding also establishes the relationship between the inner and outer rings and helps control radial runout and rotational accuracy.
For high-precision reducer bearings, the grinding process should be supported by in-process measurement and final inspection. Dimensional control alone is not sufficient. Surface condition, roundness, raceway profile, axial runout, and assembly torque may also affect performance.
Superfinishing or other fine surface-processing methods may be used where required by the application. A controlled raceway surface can reduce friction, support stable lubricant films, and limit the initiation of fatigue damage. The appropriate finish depends on bearing size, load, speed, material, lubrication, and customer requirements.
Rolling elements must be selected according to diameter variation, roundness, surface quality, and dimensional consistency. Variation among rolling elements can influence load distribution and preload. Careful matching helps ensure that the assembled bearing performs consistently.
Assembly includes cleaning, component matching, cage or separator installation where applicable, lubricant application, preload adjustment, and final rotation checks. Contamination control is essential. Small particles can create noise, increase torque, damage raceways, and reduce the service life of a precision bearing.
For rigid bearings, preload is adjusted to achieve the required combination of rigidity and smooth rotation. For flexible bearings, assembly must preserve the thin-walled structure and avoid unwanted deformation. Handling fixtures and controlled assembly procedures can reduce the risk of scratches, dents, or dimensional damage.
Quality control should continue after assembly. Depending on the product configuration and customer requirements, inspection may include dimensional measurement, radial and axial runout, rotation torque, preload verification, noise and vibration checks, visual inspection, and packaging verification.
Inspection data supports process improvement as well as product acceptance. When results are recorded across multiple production lots, engineers can identify trends in grinding accuracy, preload, torque, or dimensional stability. This data-driven approach helps reduce variation and strengthens the reliability of future production.
UKL Bearing Manufacturing Co., Ltd. operates as an integrated manufacturer and trader with an engineering and export-oriented business structure. The company provides bearings for customers in Europe, Asia, Africa, Russia, North America, and other markets. Its international experience supports communication across different technical specifications, packaging requirements, documentation systems, and delivery expectations.
The company reports a workforce of approximately 201 to 500 employees and a production capacity of about 10,000 to 50,000 units per month. This capacity provides flexibility for both recurring OEM programs and larger wholesale requirements. Production planning can be organized around different bearing sizes, product families, and customer schedules.
UKL integrates research and development with manufacturing. Its R&D activities include high-precision cross roller bearings, dual-direction thrust angular contact ball bearings, and other specialized bearing products for CNC machinery, robotics, and intelligent automation. This product knowledge is relevant to harmonic reducer applications because many of the same engineering principles apply: stiffness, controlled preload, compact design, accuracy, and long-term reliability.
The factory includes production operations covering forging, turning, heat treatment, grinding, assembly, and packaging. This broad process coverage gives the company greater control over key manufacturing variables than a supply chain that depends entirely on unrelated subcontractors. It also provides a clearer route for engineering feedback. If an issue is discovered during assembly or final inspection, the manufacturing team can investigate upstream operations more efficiently.
OEM and ODM experience is another important strength. Harmonic reducer manufacturers may require nonstandard bore dimensions, alternative mounting holes, special preload levels, customized packaging, corrosion protection, or specific inspection reports. A supplier with experience in custom bearing programs can evaluate these requirements and coordinate them with production capability.
Integrated production can improve consistency by reducing unnecessary transfers between suppliers. Every transfer creates potential variation in handling, storage, measurement methods, and process interpretation. By coordinating multiple operations within one manufacturing organization, UKL can establish common quality objectives from raw material preparation through final assembly.
Consistency is especially important for matched bearing sets and repeated robot-joint production. A customer designing a standard reducer platform expects the bearing geometry, preload, mounting interface, and rotation behavior to remain stable from batch to batch. Process documentation, inspection records, and production controls help support that expectation.
Precision bearing selection often requires technical discussion. Customers may need to provide radial load, axial load, overturning moment, speed, operating temperature, lubrication method, mounting arrangement, duty cycle, and target service life. UKL’s multilingual service team provides technical communication, installation guidance, and after-sales maintenance support for customers in different regions.
Technical support is valuable before purchase as well as after delivery. Early consultation can prevent an incorrect bearing selection, an unsuitable fit, or an avoidable mounting problem. It can also help determine whether the customer should use a standard product or request a customized design.
Industrial robot joints require compact, rigid, and repeatable transmission systems. Harmonic reducers are commonly used where high reduction ratios and low backlash are important. The associated rigid bearing supports the output arm and resists the moment generated by the payload, while the flexible bearing accommodates the motion of the harmonic generator.
In applications such as welding, palletizing, assembly, material handling, and painting, the bearing may experience frequent acceleration, deceleration, reversing motion, and varying external loads. Correct preload and installation are essential for maintaining positioning accuracy and limiting vibration.
Collaborative robots often prioritize compact size, low weight, smooth motion, and controlled force interaction. A precision harmonic reducer bearing can contribute to a lightweight joint design by combining radial, axial, and moment-supporting functions in a compact structure.
The bearing must be selected according to the robot’s payload, reach, operating speed, safety control system, and expected number of cycles. Low friction and stable rotation are also valuable because they support more predictable torque sensing and servo control.
Machine tools use precision bearings in rotary tables, indexing mechanisms, tool changers, and auxiliary axes. Accuracy and rigidity are important because movement errors can affect machining quality, surface finish, and dimensional consistency.
A crossed roller bearing may be used where the design requires a compact bearing with high resistance to moment loading. The correct bearing can help maintain the position of the rotary component while limiting deflection under cutting or indexing forces.
Aerospace mechanisms and specialized equipment often require high reliability, low mass, controlled movement, and strict documentation. Bearing selection must account for the operating environment, temperature range, vibration, lubrication, maintenance limitations, and safety requirements.
The CSF(G) series provides a range of sizes for different compact motion systems. However, aerospace and safety-critical applications require a project-specific technical review. Material certificates, inspection records, special lubrication, and additional testing may be required according to the customer’s quality system.
Automated inspection machines, semiconductor equipment, packaging systems, and precision positioning stages rely on repeatable movement. These systems may operate continuously and may be highly sensitive to vibration, contamination, and positioning drift.
A precision bearing with stable preload and accurate raceways can help provide smooth motion and predictable load support. The final performance depends on the complete assembly, including the motor, reducer, encoder, housing, lubrication system, and control software.
The first step is to identify the actual loading condition. Engineers should calculate radial load, axial load, overturning moment, shock load, and the combination of these loads during acceleration and deceleration. Static loads should be considered separately from dynamic loads because a bearing may encounter high stationary loads even when the average operating speed is low.
For robot joints, payload is only one part of the calculation. The distance from the bearing center to the payload, the weight of the arm, the acceleration profile, and external process forces can all create significant moment loading. Selecting a bearing only according to payload weight may result in an undersized design.
The bore, outside diameter, section dimensions, pitch-circle diameter, and mounting-hole specifications must match the reducer housing and output structure. The CSF(G) series includes models with different mounting patterns and, in some cases, alternative bore dimensions.
Designers should verify the complete mechanical drawing rather than relying only on nominal dimensions. Fit tolerances, shoulder dimensions, bolt clearance, bolt grade, clamping sequence, and surface flatness can affect bearing performance. Mounting surfaces should be clean, rigid, and free from burrs or distortion.
Preload improves rigidity but also affects starting torque, running torque, heat generation, and service life. The bearing supplier should receive the intended operating speed, temperature, lubricant, duty cycle, and load profile before recommending a preload condition.
If the bearing is installed in a housing that deforms during bolting, the actual preload may differ from the value measured before installation. Housing stiffness and assembly torque should therefore be considered during system validation.
Lubricant selection must match the bearing speed, load, temperature, and operating cycle. The lubricant should also be compatible with the reducer’s other components and seals. In clean-room or vacuum-related applications, special lubricants and cleaning procedures may be required.
Dust, moisture, chemical exposure, and temperature changes can reduce bearing life. Protective covers, seals, correct storage, and suitable corrosion prevention should be included in the equipment design. If a bearing will operate in a harsh environment, the customer should communicate the conditions before ordering.
Precision bearings should be handled carefully during installation. Impact loading, contamination, uneven tightening, and incorrect tooling can damage raceways or alter preload. The bearing should be pressed or clamped using the appropriate ring and should not be installed by transmitting force through the rolling elements.
Maintenance planning should include lubricant inspection, bolt inspection, noise monitoring, torque monitoring, and periodic verification of positioning accuracy. A change in operating noise, vibration, temperature, or rotational resistance can indicate contamination, insufficient lubrication, mounting distortion, or progressive damage.
Before installation, inspect the bearing, housing, shaft, flange, and mounting surfaces. Remove foreign particles, burrs, rust inhibitors that are incompatible with the lubricant, and any machining residue. Check that the mounting surfaces are flat and that the bolt holes align without forcing the components into position.
Apply the recommended lubricant in the correct quantity. Too little lubricant may increase wear and heat, while too much lubricant may increase churning resistance and operating temperature. The correct quantity depends on the bearing type, speed, internal space, and reducer design.
Install the bearing without impact. If an interference fit is used, apply force evenly to the ring being fitted. Do not apply installation force through the rollers. Use clean tools and maintain the orientation specified by the reducer design.
Tighten mounting bolts gradually in a crosswise or diagonal sequence. This helps distribute clamping force and reduces the risk of housing distortion. After tightening, rotate the bearing by hand or with a controlled low-speed drive to check for abnormal resistance, binding, or noise.
Where a preload specification is provided, verify the assembled torque or axial movement according to the agreed inspection method. The measured value should be evaluated at a controlled temperature and with the specified lubricant. If the result is outside the acceptable range, investigate the mounting surfaces, bolt sequence, fit, contamination, and component dimensions before operating the reducer.
The value of a harmonic reducer bearing is determined by more than its purchase price. A bearing that maintains accuracy and rigidity can help reduce downtime, protect adjacent components, and preserve the performance of the complete reducer. Conversely, an unsuitable or inconsistent bearing can cause difficult-to-diagnose problems throughout the motion system.
Long-term reliability begins with stable materials and continues through every production stage. Forging quality influences the ring structure. Heat treatment affects hardness and fatigue strength. Grinding determines raceway geometry and surface condition. Assembly controls preload and cleanliness. Packaging protects the completed bearing during storage and transportation.
UKL’s manufacturing structure is intended to connect these stages. The company’s production lines cover the major processes required for bearing manufacturing, while its R&D capability supports product development and application analysis. This combination is useful for customers seeking a long-term OEM or ODM partner rather than a one-time trading source.
International distribution also requires dependable packaging and documentation. Precision bearings should be protected against moisture, impact, contamination, and corrosion during transportation. Product labels, batch information, inspection documents, and installation guidance help customers manage incoming inspection and traceability.
Modern bearing production must balance performance with responsible use of materials and energy. UKL identifies sustainability as a long-term commitment and adopts environmentally responsible processes, material recycling, and energy-use optimization where possible.
Efficient production benefits both the environment and the customer. Better process control can reduce scrap, rework, and unnecessary energy consumption. Longer bearing service life can also reduce replacement frequency, maintenance interruptions, and the material required over the life of an industrial machine.
The company also supports educational and technical training initiatives intended to develop future engineering talent. This type of investment is relevant to the bearing industry because precision manufacturing depends on skilled personnel who understand metallurgy, process control, inspection, mechanical design, and application engineering.
A specialized supplier can provide more useful technical support than a source that only sells standard bearings. Harmonic reducer applications involve unusual deformation, compact interfaces, preload requirements, and combined loading. The supplier must understand the relationship between the bearing and the reducer rather than considering only the bearing’s catalog dimensions.
UKL’s experience with cross roller bearings and other precision products provides a foundation for discussing these requirements. Customers can request assistance with model selection, mounting dimensions, preload, customization, production planning, packaging, and after-sales support.
The company’s ability to serve OEM and ODM programs is also valuable for equipment manufacturers that require private-label products, customized drawings, controlled batches, or repeated supply. A successful program depends on clear technical communication, approved samples, stable production parameters, and consistent inspection criteria.
Compared with a general-purpose bearing solution, a precision harmonic reducer bearing offers a more application-oriented approach. It is designed around the needs of compact reducers, including rigidity, rotational accuracy, load support, installation efficiency, and deformation tolerance. This focus can help engineers improve the performance and reliability of the complete motion system.
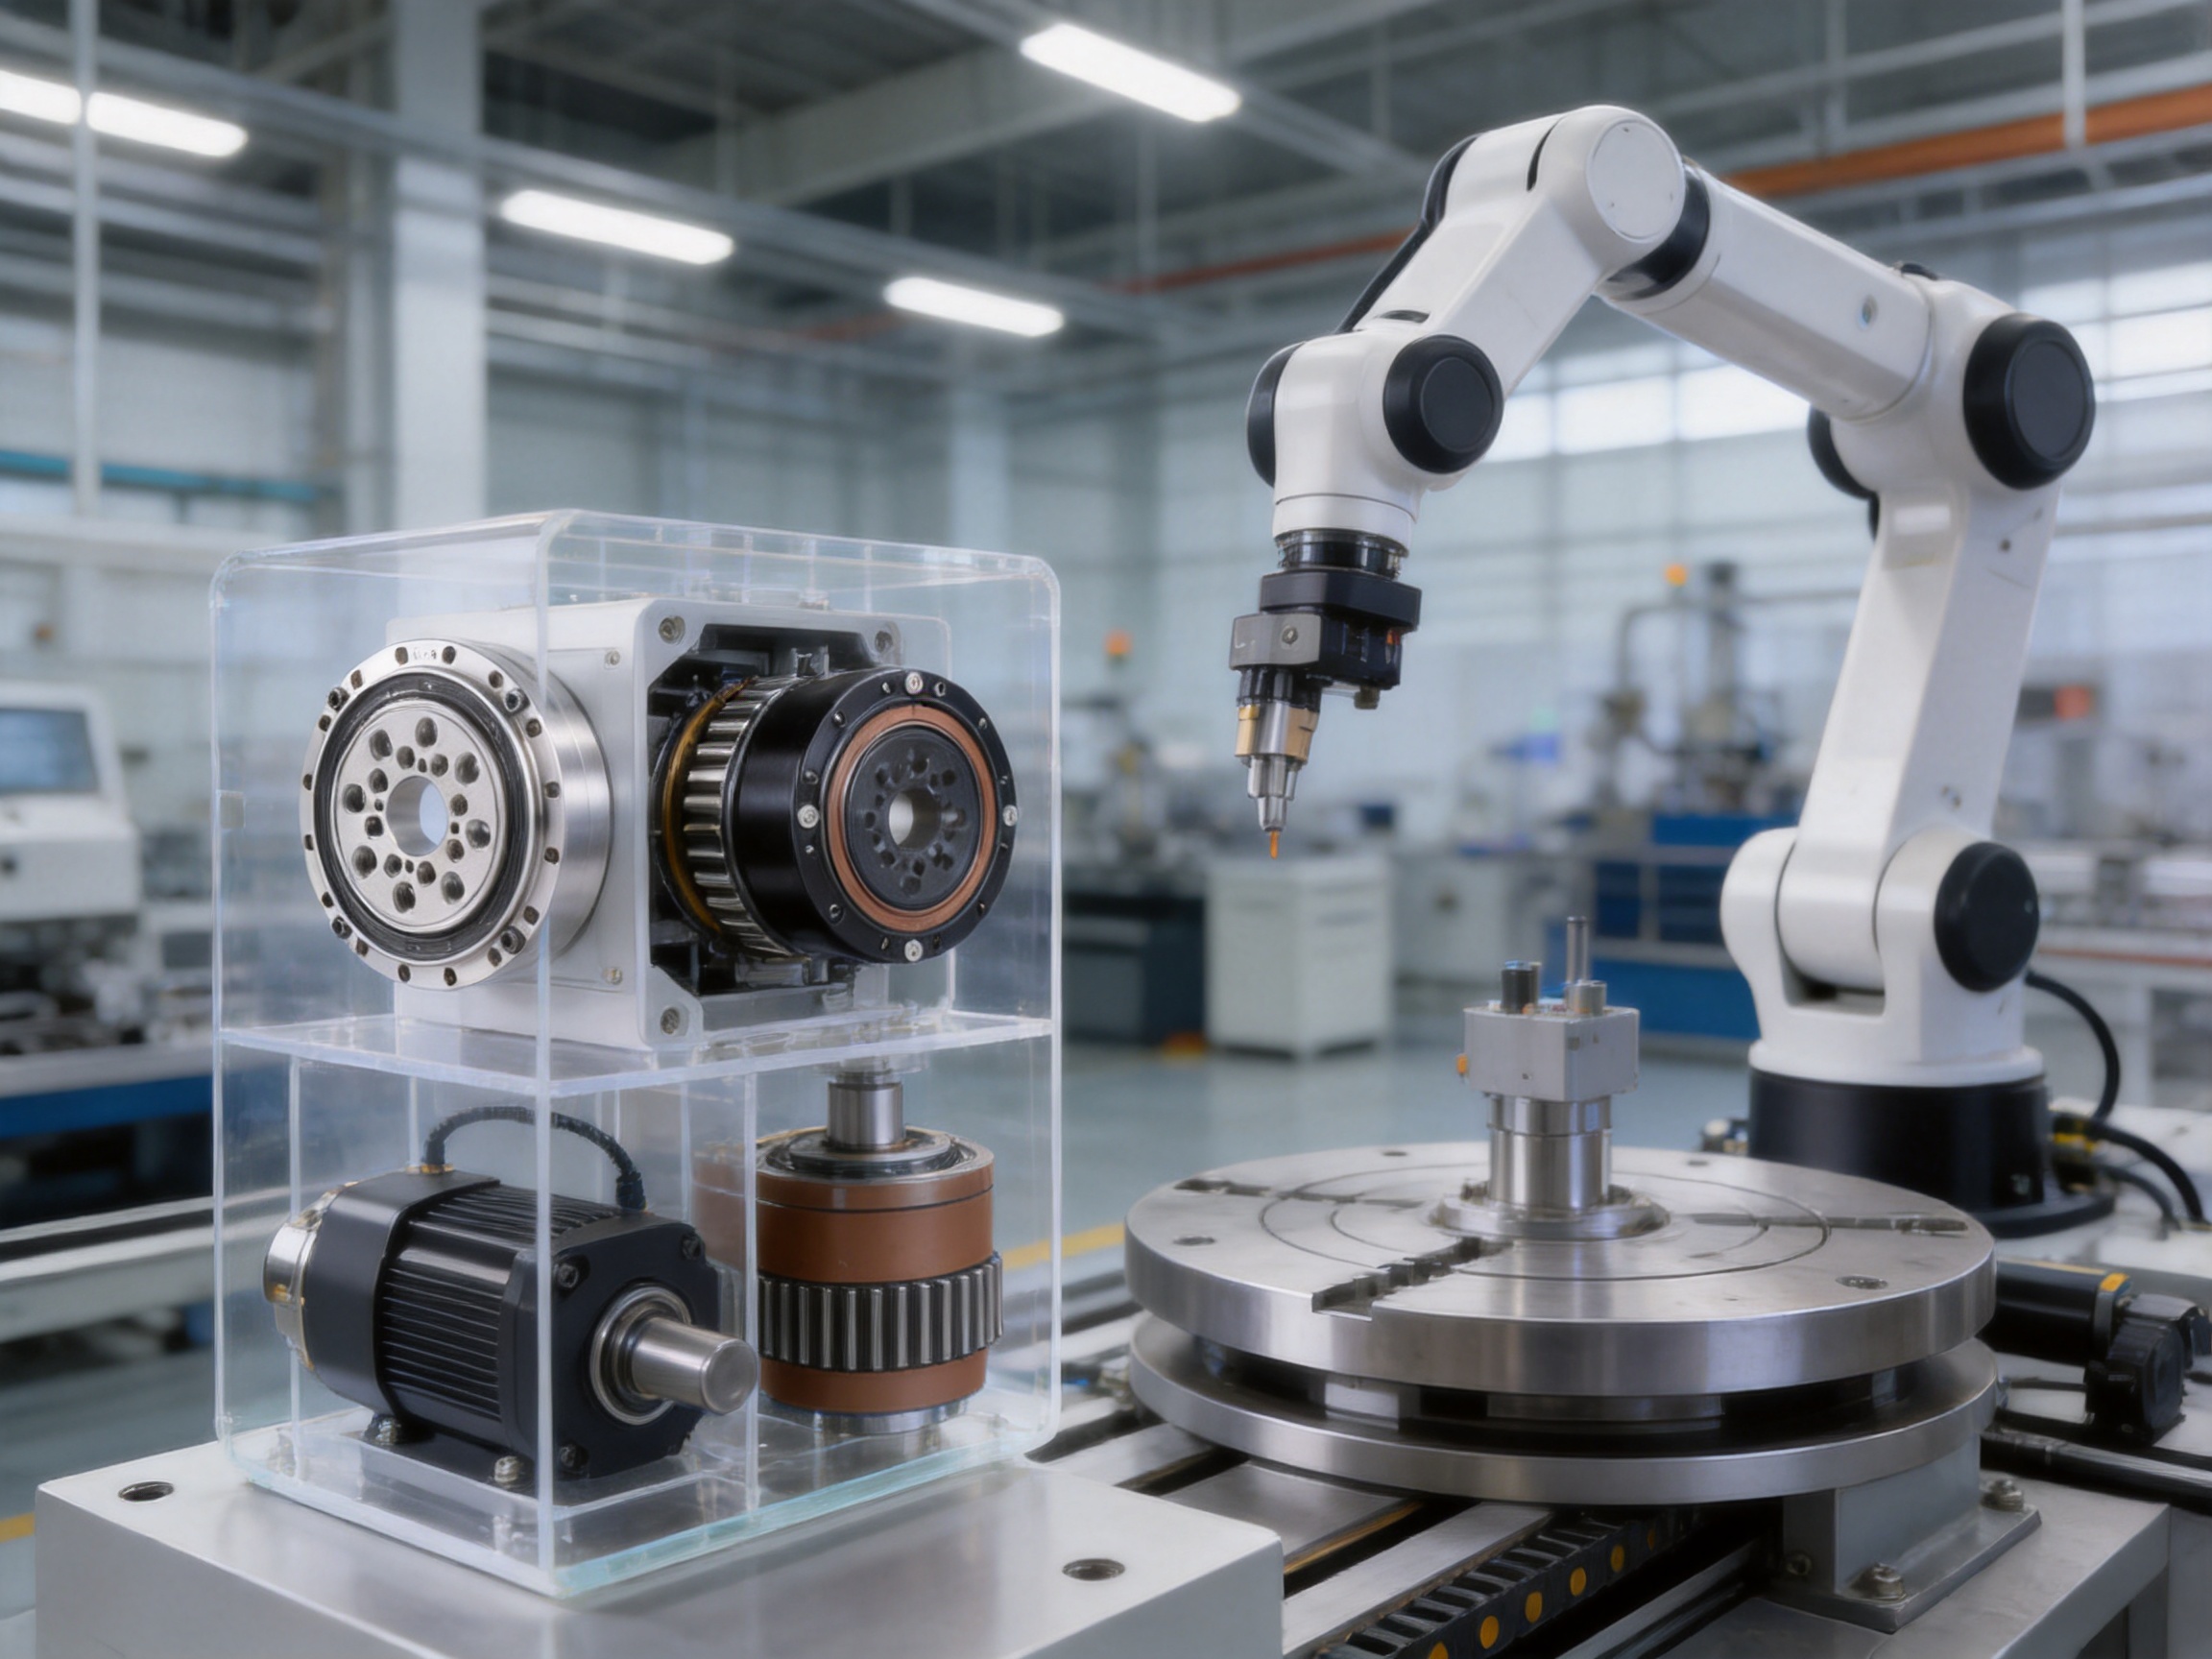
A precision harmonic reducer bearing is a bearing used within or alongside a harmonic drive transmission. It supports the reducer’s rotating and structural components while maintaining alignment, rigidity, and accurate movement. The product may serve as a rigid crossed roller bearing or as a flexible bearing designed to accommodate controlled radial deformation.
Crossed roller bearings use rollers arranged alternately at right angles. This arrangement enables the bearing to support radial loads, axial loads, and overturning moments in a compact structure. It is useful for robot joints and reducer output stages where the external load may be offset from the bearing center.
A rigid bearing is generally installed at the reducer output end and is expected to provide high stiffness, reliability, and rotational accuracy. A flexible bearing works with the elliptical cam and flexure. Its key requirement is the ability to tolerate repeated radial deformation while maintaining smooth and reliable rolling contact.
Preload removes or reduces internal clearance and improves bearing rigidity. It can help reduce unwanted movement and improve positioning accuracy. However, excessive preload can increase friction, temperature, and operating torque. The correct preload must be selected according to the load, speed, temperature, lubricant, and reducer structure.
Selection should consider the reducer interface, outside diameter, bore, section dimensions, mounting-hole pattern, radial load, axial load, overturning moment, speed, operating temperature, lubrication, and service life. The CSF(G)-14 through CSF(G)-65 models cover different dimensional and load classes. A complete technical review is recommended before final selection.
OEM and ODM customization may be available according to the required bore, mounting pattern, preload, materials, lubrication, packaging, inspection documentation, and other technical conditions. Customers should provide a drawing or complete application specification so that the manufacturing team can evaluate feasibility and establish an approved design.
Useful information includes the reducer model, bearing type, required quantity, bore and outside diameter, load conditions, speed, operating temperature, mounting arrangement, lubricant, expected service life, accuracy requirement, preload requirement, packaging standard, and delivery destination. A technical drawing or sample bearing can further improve quotation accuracy.
Service life can be improved through correct load calculation, suitable preload, clean installation, proper lubrication, adequate housing rigidity, accurate mounting, protection from contamination, and regular condition monitoring. Avoiding shock during installation and preventing uneven bolt tightening are also important.
They are intended for applications such as robotics, machine tools, aerospace equipment, and intelligent automation. The final suitability depends on the robot’s joint load, payload, speed, acceleration, duty cycle, temperature, environment, and reducer design. Application-specific verification should be completed before mass production.
The integrated production structure includes forging, turning, heat treatment, grinding, assembly, and packaging. Inspection and process control are applied throughout the production flow to support dimensional accuracy, surface quality, preload consistency, cleanliness, and reliable delivery.
Precision harmonic reducer bearings are essential to the accuracy, stiffness, and reliability of compact motion systems. Their role extends beyond simple shaft support. They help maintain the geometry of the harmonic transmission, support external loads, control output movement, and preserve stable performance during repeated operation.
The combination of crossed roller bearing technology, controlled preload, accurate raceways, compact dimensions, and multiple CSF(G) series sizes provides a strong solution for robotics, machine tools, aerospace mechanisms, and intelligent automation. Compared with general-purpose bearing arrangements, a specialized harmonic reducer bearing can simplify load support, improve structural rigidity, and make better use of limited installation space.
UKL Bearing Manufacturing Co., Ltd. strengthens this product offering through integrated manufacturing, R&D capability, OEM/ODM experience, international distribution, and technical service. Its production coverage from forging through packaging supports process coordination and traceability, while its experience with precision cross roller bearings and other specialized products helps address demanding application requirements.
For the best result, bearing selection should be completed together with the reducer design. Engineers should evaluate load, moment, speed, preload, deformation, lubrication, mounting, environment, and expected life. With the correct model and controlled installation, precision harmonic reducer bearings can provide a dependable foundation for accurate and durable motion control.
1. Harris, T. A., and Kotzalas, M. N. Rolling Bearing Analysis: Advanced Concepts of Bearing Technology.
2. International Organization for Standardization. Rolling Bearings — Dynamic Load Ratings and Rating Life.
3. International Organization for Standardization. Rolling Bearings — Static Load Ratings.
4. International Organization for Standardization. Rolling Bearings — Tolerances and Geometrical Accuracy.
5. Jones, A. B. New Departure: Ball Bearing Design and Application.
6. Manufacturer-provided CSF(G) precision harmonic reducer bearing dimensions and product information.
7. Manufacturer-provided information concerning cross roller bearings, precision bearing production, OEM/ODM services, and industrial applications.
Product Categories
Contact Us

Jane@ukl-bearing.com
Jenny@ukl-bearing.com
Andy@ukl-bearing.com
Ivy@ukl-bearing.com

+86-510- 88763239
+86-15371057968

No.1 Hehuan Road, Hudai Town, Binhu District, Wuxi City.
Ready to Begin?
Get in Touch

Now!
UKL BEARING
 English
 Español
 русский